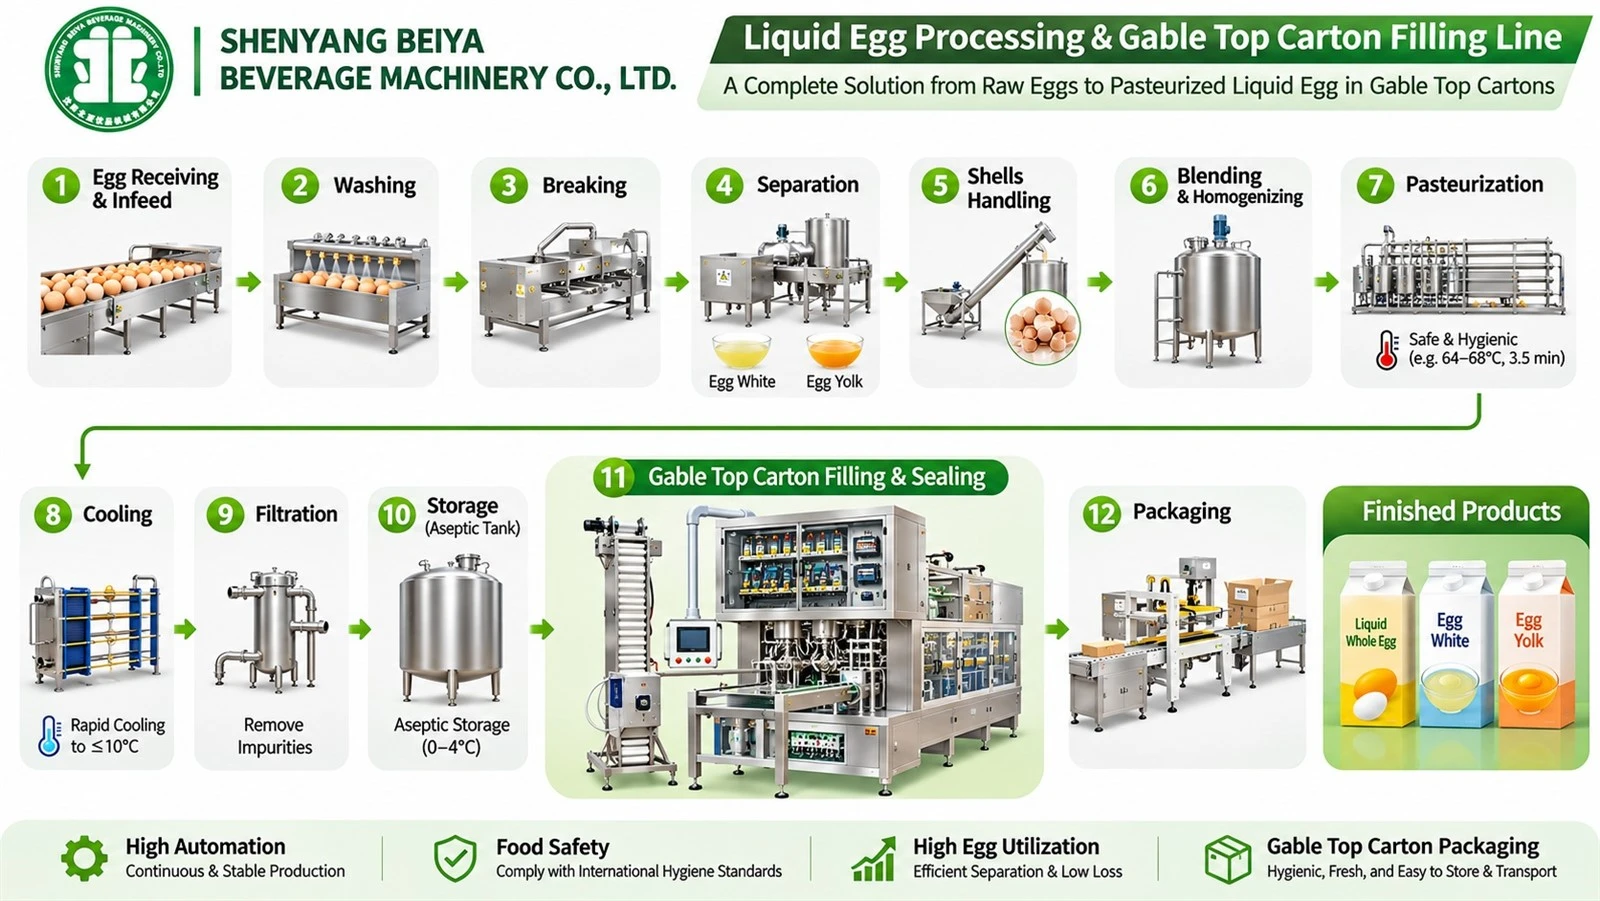

The 12-Step Process
1–2. Egg Receiving & Infeed / Washing
The line begins with gentle receiving and infeed, followed by thorough washing. Every egg is cleaned before it enters the breaking stage, removing dirt and surface contaminants to protect product safety from the very first step.
3–5. Breaking, Separation & Shell Handling
Eggs are broken automatically, then separated into egg white and egg yolk with high accuracy. Discarded shells are removed by a dedicated handling system, keeping the production area clean and maintaining a smooth, uninterrupted flow.
6–7. Blending, Homogenizing & Pasteurization
The separated liquid is blended and homogenized for consistent texture, then pasteurized at 64–68°C for about 3.5 minutes. This carefully controlled heat treatment eliminates harmful microorganisms while preserving the nutritional quality and functionality of the egg.
8–10. Cooling, Filtration & Aseptic Storage
After pasteurization, the product is rapidly cooled to ≤10°C, filtered to remove impurities, and held in aseptic storage tanks at 0–4°C. This cold chain is essential for maintaining freshness and extending shelf life before filling.
11. Gable Top Carton Filling & Sealing
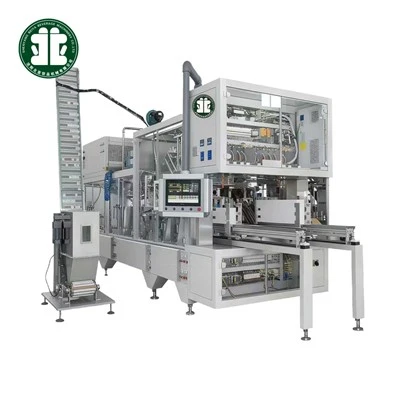
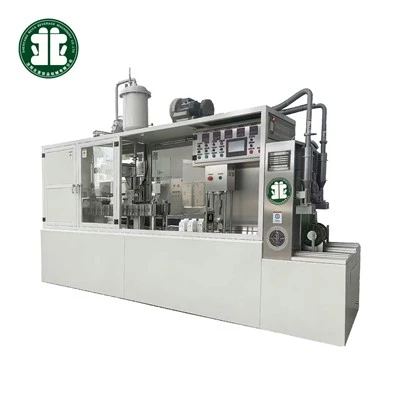
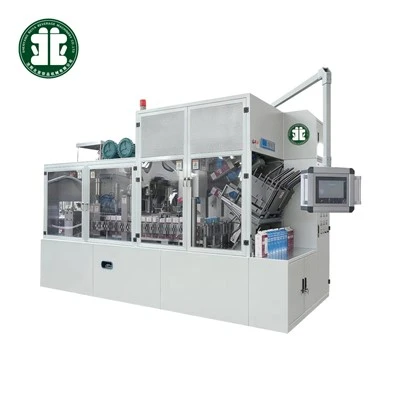
The core of the line is the gable-top aseptic filling and sealing machine. It fills the chilled liquid egg into cartons and seals them hygienically, protecting the product from recontamination and locking in freshness.
12. Packaging & Finished Products
The sealed cartons are collected and packed for shipment. The result: finished products such as liquid egg white, egg white and egg yolk in clean, shelf-ready gable-top cartons.
Why This Line Stands Out
High Automation - Continuous, stable production with minimal manual intervention.
Food Safety - Designed to comply with international hygiene standards at every stage.
High Egg Utilization - Efficient separation and low loss mean more usable product from every egg.
Gable Top Carton Packaging - Hygienic, fresh, easy to store and convenient to transport.
The Value of Gable Top Cartons
For liquid egg, packaging is part of the product. Gable-top cartons are lightweight, stackable and tamper-evident, with excellent barrier protection. They keep the product fresh without refrigeration abuse, give buyers clear labeling space, and are far easier to handle than fragile shell eggs or bulky containers - a real advantage for retailers, food-service operators and consumers alike.
Final Thoughts
A complete liquid egg line is more than a set of machines; it is a carefully engineered chain where every step protects the next. From washing and separation to pasteurization, aseptic storage and final filling, each stage is designed to deliver a safer, longer-lasting and more convenient product.
If you are planning a liquid egg project - whether for egg white, yolk or blended products - a well-integrated gable-top filling line can turn a fragile raw ingredient into a high-value, shelf-ready product.
Looking for a complete solution? Shenyang Beiya Beverage Machinery Co., Ltd. designs and supplies full liquid egg processing and gable-top carton filling lines. Contact our team to discuss your capacity, layout and packaging requirements.